Top Trusted Heavy Gauge Stamping Factories & Exporter
Industrial Whitepaper & Technical Procurement Guide: High-Tonnage Forming, Multi-Stage Deep Drawing, and Global Supply Chain Excellence for Mission-Critical Engineering.
Precision Engineering Portfolio
Engineered Heavy Gauge & Deep Drawn Components
Explore our verified production capabilities spanning structural heavy stamping, precision perforated screens, hydraulic mass transfer columns, and custom industrial filtration assemblies.
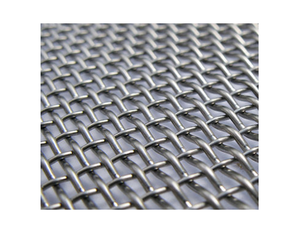
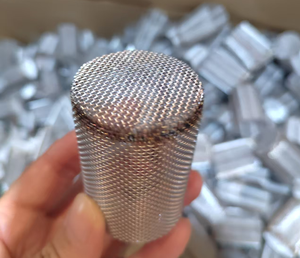
Engineered from SS304/316L alloys featuring consistent aperture geometry, high tensile resistance against mechanical backwashing, and precise metallurgical weave stability under hydraulic shear.
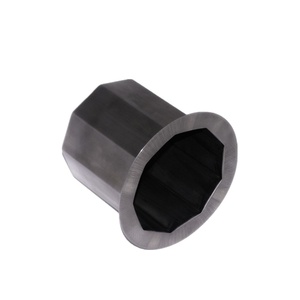
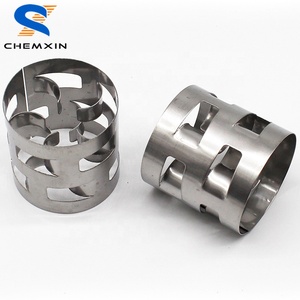
Seamless monolithic cylindrical enclosures drawn with tight wall-thickness tolerances, zero seam leakage, controlled grain stretching, and high resistance to dynamic fluid pressure vessels.
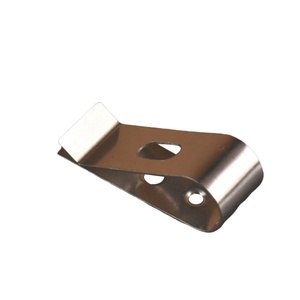
Custom high-load mounting hardware, brackets, and structural heavy-gauge stamped fittings processed through automated progressive dies with micrometer-level dimensional consistency.
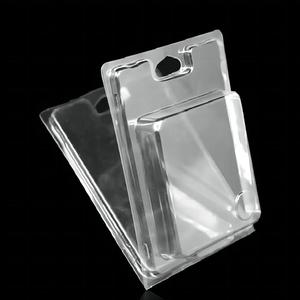
High-impact protective thermoformed nesting designed for export transit security of delicate stamped parts, machined inserts, and sensitive electronic contact pins.
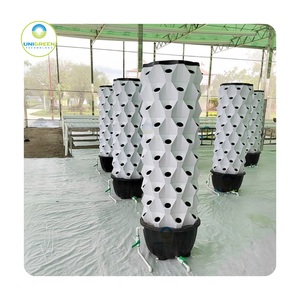
Engineered modular vertical liquid-flow columns manufactured from food-grade polymers with UV stabilizers, integrating fluid distribution geometries derived from mass-transfer design.
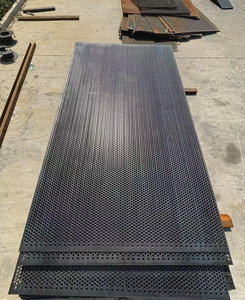
Specialized heavy-plate punching process ensuring zero burr propagation and micro-crack prevention along hole peripheries under cyclical dynamic stress and vibrational separation.
Heavy Gauge Metal Stamping: Metallurgical Mechanics, Tooling Dynamics, and Quality Assurance
In modern industrial manufacturing, heavy gauge metal stamping—generally categorized as cold forming of sheet and plate thicknesses exceeding 3.5 mm up to 20.0 mm—represents one of the most mechanically demanding niches of structural metallurgy. Unlike light stamping, where deformation stresses remain localized and material yield forces are relatively modest, heavy gauge blanking, piercing, bending, and deep drawing require enormous machine tonnage, specialized tooling steels, precise heat dissipation, and advanced finite element springback modeling. As an internationally recognized manufacturing authority established in 1998, Ambani Metals has developed comprehensive operational protocols designed to mitigate shear edge strain hardening, delamination, and premature tool chipping across aggressive production cycles.
Key Engineering Finding: In thick structural plate stamping, material fracture behavior switches from ductile plastic deformation to brittle shear propagation along the blanked cut line when die clearance falls below 8% or exceeds 16% of sheet thickness ($t$). Precise punch-die clearance optimization directly prevents microscopic burr formation and edge micro-cracks that compromise structural fatigue life in high-vibration applications.
Technical Comparison: Heavy Gauge Stamping vs. Medium Stamping vs. Fine Blanking
Selecting the optimal forming technology demands balancing raw material thickness, cut edge quality, structural integrity, and tooling cost amortized over total production volumes. The following data visualization matrix details key mechanical differentiators:
Engineering Attribute
Heavy Gauge Stamping (>4.0mm)
Standard Stamping (<3.5mm)
Fineblanking Process
Plate Thickness Capability
4.0 mm – 20.0 mm
0.4 mm – 3.2 mm
1.0 mm – 12.0 mm
Typical Press Force Range
400 to 2,500 Metric Tons
45 to 350 Metric Tons
100 to 1,200 Metric Tons (Triple Action)
Cut Edge Characteristic
1/3 Rollover & Burnish, 2/3 Clean Fracture
1/2 Burnish, 1/2 Fracture Zone
100% Fully Burnished, Zero Fracture Edge
Tool Steel Requirement
DC53, Caldie, Cr8Mo2SiV, Matrix High-Yield
D2, SKD11, High Carbon Cold-Work Alloys
High-Wear Powder Metallurgy (ASP23 / Vanadis 4)
Springback Compensation
High Elastic Stress; FEA Multi-Radius Crowning
Moderate; Standard Over-bending Dies
Minimal; Continuous Clamping & V-Ring Impingement
Secondary Finishing Needs
Deburring / Tumbling for sharp fracture edges
Minimal deburring on standard tolerances
Zero secondary shaving or edge grinding needed
Key Industrial Applications
Heavy truck chassis, pressure internals, brackets
Consumer enclosures, terminal tabs, brackets
Automotive gear selectors, clutches, locks
Deep Drawing Kinetics in Heavy Austenitic Stainless Steel
When drawing seamless cylinders—such as our deep-drawn SUS304 and 316L shells—the engineering challenge revolves around the Limiting Draw Ratio (LDR) and work-hardening kinetics. Austenitic stainless steels undergo strain-induced martensitic transformation during multi-pass cold reduction. As the blank is forced through the die cavity by the punch nose, severe hoop compression occurs in the flange area, generating high tangential stresses that induce wrinkling if blank holder pressure (BHP) is insufficient, or flange tearing if BHP is excessively high.
To overcome this, Ambani Metals utilizes segmented hydraulic cushioning with nitrogen gas manifolds, paired with multi-stage drawing dies that systematically vary the clearance-to-thickness ratio ($c/t = 1.07 \text{ to } 1.15$). Between successive reductions, precision in-line induction annealing or vacuum solution annealing at 1,050°C dissolves newly precipitated carbide phases and recrystallizes the austenitic matrix, completely restoring ductility for subsequent redrawing passes without risk of delayed longitudinal cracking (season cracking).
Future Procurement Trends in Global Heavy Stamping (2025–2030)
Procurement directors and supply chain engineers are confronting rapid transformations across environmental sustainability mandates, material lightweighting, and lead-time constraints. Navigating vendor selection over the coming decade requires evaluating factories against these emerging technical shifts:
Shift to UHSS & AHSS Alloys
OEMs are transitioning from conventional mild plate to Advanced High-Strength Steels (DP780, CP1000) and high-yield stainless alloys to decrease component mass while maintaining crash and load ratings. This shift requires factories equipped with high-rigidity servo presses to manage extreme springback.
Near-Net-Shape Cold Extrusion
To eliminate costly multi-axis CNC secondary machining, modern procurement prioritizes suppliers that combine heavy gauge stamping with progressive cold forging, yielding near-net-shape splines, serrated bosses, and countersinks directly within the press tool.
Green Metallurgy & Carbon Footprint Tracking
Global tier-one contractors now require mill-level heat certificate traceability, ISO 14064 carbon disclosure, and high scrap utilization rates. Factories with established secondary scrap-closed-loop logistics offer distinct regulatory advantages across the EU and North America.
The era of conventional mechanical flywheel stamping is giving way to intelligent forming centers. Leading manufacturers invest heavily in three transformative technological domains:
1. Servo-Mechanical Motion Profiling: By decoupling slide velocity from traditional crankshaft rotation, high-tonnage servo presses allow programmed deceleration immediately prior to punch impact. This minimizes shock vibration, eliminates micro-cracking in thick stainless plates, and enhances formability during deep draw strokes.
2. In-Die Piezoelectric Acoustic Sensors: Continuous real-time monitoring of punch force signatures detects minute deviations in stock thickness, die galling, or slug-pulling occurrences before physical tooling failure happens, safeguarding production schedules on massive 100,000+ unit runs.
3. Dynaform / AutoForm Virtual Tool Simulation: Full digital twin validation prior to physical tool steel cutting reduces prototype commissioning loops from months to days, pinpointing potential thinning, wrinkling, and localized strain concentrations.
Factory Qualifications & Authority
Why Global Engineering EPCs Partner with Ambani Metals
Founded in 1998, Ambani Metals combines quarter-century forming expertise with an integrated supply chain spanning heavy stamping, column internals, industrial mesh, and specialty alloy inventories.
Full Heat-Number Traceability
Every batch of raw coil and plate is mill-sourced from tier-one steelworks with complete EN 10204 3.1 chemical and mechanical inspection certificates verified by Spectro-analysis.
Complete In-House Tooling Lifecycle
In-house tooling center equipped with slow-feeding wire EDMs, 5-axis CNC machining centers, and vacuum heat-treatment furnaces to guarantee proprietary tool longevity and revision control.
Metrology & Quality Laboratory
Hexagon Coordinate Measuring Machines (CMM), optical 3D surface scanners, micro-hardness testers, and hydrostatic leak testing ensure zero defect escape to international job sites.
Global Multi-Port Export Logistics
Exporting across 20+ countries—including the United States, Canada, Australia, the UAE, Saudi Arabia, and Germany—utilizing ISPM-15 compliant seaworthy crating and export customs clearance.
Procurement Knowledge Base
Frequently Asked Questions for Engineering & Procurement Teams
Straightforward answers regarding tooling feasibility, material behaviors, quality compliance, and export ordering protocols.
What is the maximum material thickness and press capacity available for heavy stamping?
Our fabrication lines operate mechanical and hydraulic stamping presses ranging from 400 tons up to 2,500 metric tons. We routinely process heavy gauge carbon steel up to 20.0 mm thickness, austenitic stainless steels (SUS304, SUS316L) up to 14.0 mm thickness, and high-strength nickel alloys up to 10.0 mm thickness across single-operation and progressive production modes.
How do you resolve edge micro-cracking and high burr formation on thick pierced plates?
Cut-edge defects in heavy gauge materials stem from improper punch-die clearance and tool deflection. We calculate custom clearance envelopes based on real ultimate shear strength ($\tau = 0.8 \times \sigma_b$), generally maintaining punch-die clearance between 10% and 14% of nominal sheet thickness. Combined with precision tool steels (DC53 or powdered metallurgy), nitrogen stripper plates, and controlled shear angle grinding on punches, this completely eliminates micro-fissuring and limits burr height to under 5% of material thickness.
Can you manufacture deep drawn stainless steel shells without intermediate annealing?
The feasibility of drawing without inter-stage annealing depends entirely on the drawing ratio ($m = d / D$). For moderate depths where the drawing coefficient remains above $m_1 = 0.52$, we utilize high-lubricity chlorinated or synthetic boundary ester polymers to successfully draw shells in one stroke. However, for deep cylinders with large aspect ratios, intermediate vacuum solution annealing (1,050°C with nitrogen quench) is mandated to relieve strain-induced martensitic stress and avert delayed cracking.
What documentation and quality certifications accompany international shipments?
Every export order is accompanied by a comprehensive Quality Dossier containing: EN 10204 3.1 Material Test Certificates (traceable by cast/heat number), CMM Dimensional Inspection Reports with First Article Inspection (FAI) per AS9102 or PPAP Level 3 standards, surface roughness (Ra) records, ultrasonic test reports (where requested), and fumigation certificates for sea-freight wooden packaging.
What engineering inputs are required to receive a formal tooling and piece-part quotation?
To prepare an accurate engineering quote, we request: 2D mechanical drawings with geometric dimensioning & tolerancing (GD&T) in PDF/DWG format, 3D CAD files (STEP, IGES, or Parasolid), specified material grade and standard (e.g., ASTM A240 SS316L, DIN 1.4404), projected annual volume (EAU), packaging constraints, and the designated destination seaport or airport.
Initiate Your Engineering Review & Heavy Stamping Quote
Connect directly with Ambani Metals' senior tool designers and export metallurgists. We offer technical DFM feedback, tonnage analysis, and rapid turn-around cost proposals tailored to your application.