 SS 304 / 316

- +91-9930498858Call / WhatsApp
- [email protected]Email Us
From micro-tolerance seamless stainless steel cylinders to progressive die enclosures and heavy-duty separation media, explore our high-precision product portfolio engineered to exceed rigorous California industrial specifications.
SS 304 / 316
 Modular Enclosure
 High Purity 316L
 Demister Elements
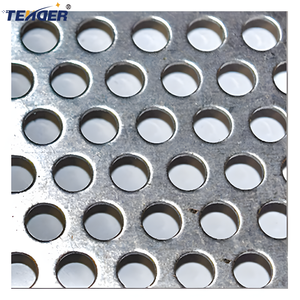 Architectural Grade
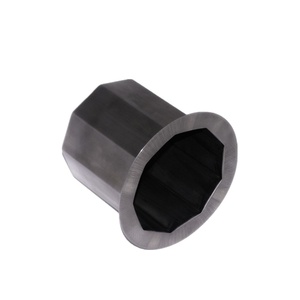 Deep Drawn Seamless
 CNC & Stamping
 Multi-Stage Drawing
An advanced engineering review on cold forming mechanics, limiting draw ratios (LDR), and microstructural evolution for engineers and procurement specialists across the Greater Los Angeles industrial corridor.
The transition of flat sheet blanks into high-depth aspect cylinders requires precise management of the Limiting Draw Ratio (LDR = Blank Diameter / Punch Diameter). Through optimized blank holder forces (BHF) and intermediate vacuum annealing, our mechanical transfer presses exceed standard LDR benchmarks (achieving up to 2.2 on first draws and over 3.4 in progressive multi-stage redrawing), eliminating common defects like flange wrinkling, earring, and longitudinal sidewall tearing.
Metals such as austenitic stainless steel (SUS304, SUS316L) undergo severe strain hardening during cold metal displacement, where martensitic transformation increases mechanical tensile strength while reducing elongation. We incorporate precise induction and controlled atmosphere bright annealing cycles at 1050°C–1100°C. This relieves internal residual shear stresses, restores uniform equiaxed austenite grain size (ASTM 7–8), and retains optimal ductility for secondary necking, curling, and piercing operations.
Galling and metal pickup represent major failure mechanisms when drawing high-strength alloys. Our tooling utilizes premium grade tungsten carbide dies and hardened tool steels (SKD11, D2) coated with Physical Vapor Deposition (PVD) titanium carbo-nitride (TiCN) and diamond-like carbon (DLC). Coupled with high-pressure synthetic boundary lubricants, our deep drawing tooling provides mirror-polished inner wall finishes down to Ra 0.2 μm without secondary honing.
From South Bay's aerospace giants to the burgeoning CleanTech corridor in Downtown LA and medical robotics hubs in Orange County, deep drawn metal stamping plays an irreplaceable role in modern California manufacturing.
Centered around El Segundo, Hawthorne, and Long Beach, private space and defense contractors demand hermetically sealed, lightweight, and ultra-high-strength components. Our deep drawn stainless steel and Inconel can assemblies serve as high-pressure rocket propellant valve covers, sensor shields, and cryogenic fluid enclosures that endure extreme vibration and thermal shock.
Across the Los Angeles Basin, the electric vehicle revolution drives unprecedented demand for precision prismatic and cylindrical battery canisters, capacitor housings, and heat exchanger manifolds. High-speed progressive draw tooling delivers thin-wall deep drawn aluminum and nickel-plated steel cans with uniform wall thicknesses down to ±0.015 mm.
Southern California's critical refining infrastructure, stretching from Wilmington to El Segundo, relies on corrosion-resistant separation internals. We integrate deep drawn bubble caps, valve trays, and custom wire mesh demister elements capable of operating continuously in acidic H2S, sour gas, and high-chloride marine environments.
Biomedical innovators in Irvine, Pasadena, and the greater LA health sciences corridor require micro-deep drawn sensor capsules, surgical instrument sleeves, and implantable grade titanium enclosures. Seamless construction eliminates micro-crevices, preventing bacterial colonization and ensuring complete passivation compliance.
The entertainment production capital relies on robust, aesthetically flawless thermal housings for high-power LED cinematography fixtures, parabolic reflector housings, and audio acoustics. Deep drawn seamless aluminum reflectors provide maximum thermal dissipation and flawless optical symmetry for studio lighting.
Addressing California's strict water sustainability targets, regional reverse osmosis and industrial water treatment installations utilize our seamless stainless steel filter vessels, perforated core tubes, and wire mesh filtration cartridges designed for uninterrupted service against coastal saline corrosion.
Selecting the ideal metal alloy requires balancing work hardening exponents (n-value), plastic strain ratios (r-value), and operating environment resilience.
| Alloy Family & Grade | Drawability Index (n / r value) | Tensile / Yield Strength (MPa) | Corrosion & Thermal Resistance | Primary Los Angeles Applications |
|---|---|---|---|---|
| Austenitic Stainless (304 / 304L) | n ≈ 0.45 / r ≈ 1.05 (High work-hardening, excellent elongation) | 515 UTS / 205 YS | Excellent atmospheric and organic acid resistance; up to 870°C | Pressure canisters, sensor enclosures, food-grade processing cans, HVAC fluid caps. |
| Molybdenum Stainless (316 / 316L) | n ≈ 0.40 / r ≈ 1.00 (Superior drawing ductility with low carbon) | 485 UTS / 170 YS | Outstanding chloride pitting resistance; ideal for coastal Pacific exposure | Marine hardware, reverse osmosis filter housings, API pharmaceutical separation vessels. |
| Nickel Superalloy (Hastelloy C-276) | n ≈ 0.38 / r ≈ 0.95 (Requires multi-stage hydraulic redraws) | 790 UTS / 355 YS | Extreme wet chlorine, hypochlorite, and sulfuric acid resistance to 1040°C | Chemical synthesis scrubbers, petrochemical catalyst trays, specialized defense ordnance. |
| Nickel-Copper (Monel 400) | n ≈ 0.32 / r ≈ 1.10 (Smooth drawing with moderate strain hardening) | 550 UTS / 240 YS | Immune to chloride stress corrosion cracking; excellent in fast-flowing seawater | Port of LA maritime instrumentation, offshore valves, refinery hydrofluoric acid alkylation. |
| Deep Draw Aluminum (3003 / 5052-O) | n ≈ 0.28 / r ≈ 0.75 (Superior cold flow, minimal tool friction) | 190 UTS / 75 YS | High strength-to-weight ratio; good saltwater spray tolerance; anodizable | EV battery module enclosures, avionics shielding cans, aerospace ducting shells. |
| High Purity Copper & Brass (C26000) | n ≈ 0.42 / r ≈ 0.90 (Classic 70/30 cartridge brass, highest ductility) | 340 UTS / 110 YS | High electrical and thermal conductivity; natural antimicrobial surface | RF/EMI shielding cans, oxygen apparatus components, electronic terminal housings. |
How Los Angeles manufacturing executives balance localized speed-to-market with international cost efficiencies and raw material volatility.
Situated directly at the maritime trade terminus of North America, Los Angeles manufacturers face unique supply chain realities. Forward-thinking procurement teams utilize our strategic direct-port delivery framework. By landing precision deep drawn components at the San Pedro Bay port complex, Tier-1 aerospace and automotive buyers bypass inland rail bottlenecks, shaving 10 to 14 days off domestic shipping transit times.
Running high-tonnage mechanical and hydraulic press rooms inside the Los Angeles-Long Beach-Anaheim metropolitan zone involves skyrocketing industrial real estate leases, intense AQMD environmental permitting, and rising kilowatt-hour electricity rates. We offer a proven hybrid sourcing model: complete CAD/CAM tool design and initial pilot qualification backed by cost-competitive, high-volume production facilities.
Defense and NewSpace operations in El Segundo and Torrance cannot compromise on compliance. Every deep drawn batch is dispatched with complete Mill Test Certificates (MTC 3.1) showing full heat number traceability, positive material identification (XRF PMI testing), and Coordinate Measuring Machine (CMM) dimensional verification charts ensuring full alignment with AS9100 and ISO standards.
From single-stage prototypes to continuous progressive-die stamped assemblies, Ambani Metals combines in-house tool & die engineering with international export compliance.
Complete CAD/CAM tooling design, wire EDM, and CNC milling under one roof. We optimize draw radii, blanking clearances, and stage progressions to guarantee dimensional repeatability.
Proven mastery forming challenging high-nickel, non-ferrous, and reactive metals, including Monel, Inconel, Hastelloy, Titanium, Brass, and high-purity Austenitic Stainless 316L.
Seamless integration of in-line punching, sidewall trimming, beading, roll threading, brazing, TIG/laser welding, and sanitary electropolishing for turnkey part delivery.
Over two decades exporting heavy industrial mass transfer hardware, wire mesh filters, and deep drawn components to 20+ countries, including the United States, UAE, and Canada.
Technical clarifications on deep draw tooling lead times, dimensional tolerances, material certifications, and shipping into Southern California.
For custom deep drawn tooling (progressive die sets or multi-stage transfer tooling), standard lead time ranges from 3 to 5 weeks depending on part complexity, depth-to-diameter ratio, and material type. First Article Inspection (FAI) samples with full CMM inspection reports are dispatched via express air freight directly to your California facility for benchtop and functional verification before mass production release.
During deep drawing, sheet metal naturally thickens near the open flange and thins near the punch radius. We control this variation through precision-engineered ironing dies that calibrate the annular gap between punch and die ring. This ensures outer and inner diameter tolerances within ±0.025 mm (±0.001 in) and circularity/runout within 0.05 mm, fully satisfying aerospace sensor canister requirements.
Yes. Every shipment includes certified EN 10204 Type 3.1 Mill Test Certificates (MTC) detailing complete chemical composition (spectrographic analysis) and mechanical properties (Yield, Tensile, Elongation, Hardness). Furthermore, our stainless steels and specialty alloys are 100% melt-traceable, ensuring compliance with US defense, ASME boiler, and pressure vessel specifications.
While CNC billet machining creates substantial material scrap (often 60%–80% waste on hollow cylinders) and metal spinning is limited to low cycle rates, deep drawing provides a rapid cycle time (up to 40–60 strokes/minute on automated transfer presses) with near-zero material loss. For annual production volumes exceeding 2,500 to 5,000 units, the initial tooling cost is rapidly amortized, slashing piece prices by up to 65%.
Export packaging complies with international phytosanitary ISPM-15 standards. Drawn parts are individually partitioned using thermoformed blister trays, anti-scratch cell separators, and sealed vapor corrosion inhibitor (VCI) bags with desiccant pouches. Goods are packed in heavy-duty reinforced wooden crates or steel-strapped pallets engineered to withstand ocean transit and cross-docking at the Port of Long Beach.
Collaborate with our senior tooling engineers. Submit your 2D/3D CAD models (STEP, IGES, DXF) or process data sheet today for an in-depth manufacturing feasibility review and competitive FOB/DDP Los Angeles commercial proposal.