Top China Deep Drawn Parts Manufacturer & Factories in London
High-Precision Deep Drawing, Progressive Tooling & Custom Sheet Metal Forming Engineered for Greater London & UK Tier-1 Industrial Applications
Precision Metal Forming Systems
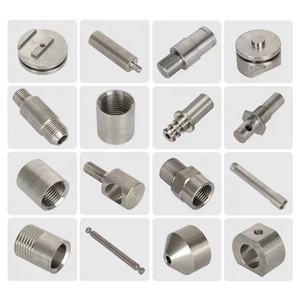
Featured Deep Drawn, Stamped & High-Tolerance Enclosure Assemblies
Integrating high-tonnage hydraulic deep drawing presses, multi-stage progressive stamping dies, and full material test certification (MTC 3.1) to meet stringent UK and European mechanical tolerance standards.
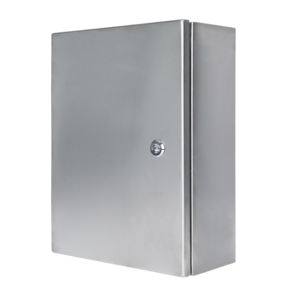
Heavy-duty 304/316 sealed enclosures, deep drawn and formed with polyurethane robot-poured foam gaskets for London transportation and trackside IoT nodes.
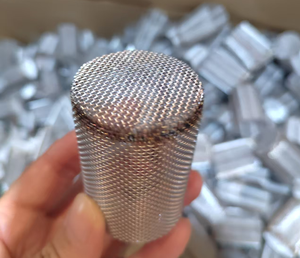
Precision calibrated cylindrical filter elements with micro-mesh diffusion layers and deep drawn protective end-caps for high differential pressure systems.
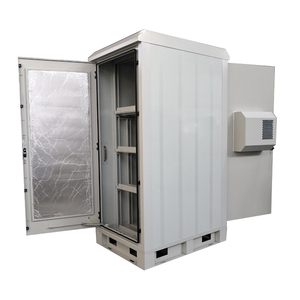
Engineered outdoor energy storage cabinet with thermal management, deep-stamped structural louvers, and reinforced stainless framework for urban substations.
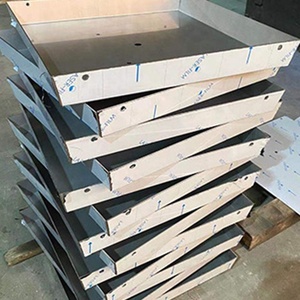
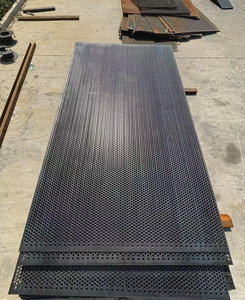
Stress-relieved one-piece stamped screen plates exhibiting zero edge micro-cracking; optimized for chemical distillation column trays and industrial sifters.
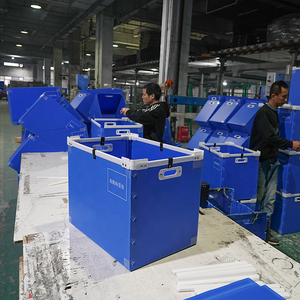
Durable, returnable transit packaging designed to protect mirror-finish and high-spec deep drawn metal components during global maritime and overland shipping.
Deep Drawing Metallurgy: Bridging China Production Scale with London Engineering Hubs
The manufacturing of deep drawn parts requires absolute mastery of metal plastic deformation and work-hardening kinetics. In cold-forming operations where the depth of the drawn component exceeds its radial diameter (L/D > 1.5), metal flow must be controlled under precise hydraulic blank-holder pressures. Sourcing deep drawn components from high-capability Chinese manufacturing plants gives engineering teams across Greater London, the M4 Tech Corridor, and the wider Thames Estuary significant cost advantages without sacrificing tight mechanical tolerances.
By integrating advanced finite element simulation software (AutoForm and Dynaform) at our tooling design centers, we predict localized thinning, wrinkling, and residual stress concentrations before machining tool steels (SKD11, Cr12MoV, tungsten carbide). Whether drawing austenitic stainless steels (304, 316L) with high work-hardening rates, high-conductivity oxygen-free copper (C10200), or lightweight aluminum (5052, 6061-O), our production lines maintain uniform wall thickness and geometric tolerances down to ±0.015mm, fully aligned with British Standard BS EN ISO 2768.
Multi-Stage Annealing
Intermediate hydrogen-atmosphere furnace annealing prevents stress-corrosion cracking and eliminates strain-hardening in high-draw austenitic alloys.
In-Die Sensor Feeds
Real-time optical and piezoelectric tonnage monitors prevent micro-fissuring, ensuring zero defect escapes across 100,000+ unit repeat batch orders.
Electropolishing & Passivation
Automated cleanroom passivation lines guarantee particulate-free internal surfaces conforming strictly to ASTM A967 and ISO 14644-1 requirements.
Localised Application Scenarios Across Greater London & the South East
London acts as an international headquarters and high-value design ecosystem. While heavy manufacturing has moved outwards, specialized industrial design, rapid testing, and critical infrastructure maintenance remain anchored around the Capital.
Target Sector (London & SE)
Critical Component Types
Primary Material Grades
Engineering Standards & Certifications
MedTech & Life Sciences White City, King's Cross, London BioScience
BS EN 61000-6-3 (EMC), RoHS Directive 2011/65/EU, REACH compliance
Emerging Trends in UK Precision Deep Drawn Sourcing (2025–2030)
Procurement directors and design heads in London face evolving trade regulations, including the UK Carbon Border Adjustment Mechanism (CBAM), rising energy costs, and the need for shorter concept-to-market cycles.
1. Conversion of Multi-Piece Welded Parts to One-Piece Deep Drawn Geometries: London-based OEMs are increasingly re-engineering machined castings and multi-part welded assemblies into monolithic deep-drawn structures. This transition cuts unit component weight by 30% to 55%, removes leak paths in hermetic sensor housings, and eliminates non-destructive ultrasonic weld inspection costs.
2. Hybrid Supply Chains (China Production + London Buffer Stocking): To insulate assembly schedules from shipping variability, Tier-1 system builders leverage high-volume tooling runs in our Chinese facilities while holding 30 to 60 days of Kanban safety stock in logistics warehouses around the London Orbital (M25) corridor, balancing competitive piece costs with reliable, short-lead delivery.
3. Low-Carbon Metallurgy & Material Traceability: Under UK CBAM mandates, enterprise supply chains require strict Scope 1, 2, and 3 carbon accounting. Our production lines use electric servo-press systems and mill-certified sustainably melted coil stock, providing fully traceable heat sheets and carbon declarations with every dispatch.
Factory Credibility & Scale
Built on 25+ Years of Engineering Rigor & Global Traceability
From raw coil slitting to precision progressive drawing, surface treatment, and bonded transit packaging—every stage of our process is managed under rigorous in-house quality controls.
Mill-Certified Alloys
100% material traceability from certified mills. EN 10204 3.1 Material Test Certificates (chemical composition and tensile elongation) accompany every shipment.
Full Tooling Ownership
In-house CNC, wire-cut EDM, and die-tryout presses. Tooling designs and progressive dies remain customer-dedicated with documented lifespan warranties.
CMM Metric Metrology
Comprehensive geometric inspections utilizing automated 3D Coordinate Measuring Machines, optical laser scanners, and concentricity gauges down to ±0.005mm.
London Door-To-Door Logistics
DDP delivery service directly into London, Kent, Surrey, and Essex manufacturing sites. Full customs clearance handling, marine insurance, and zero import hassles.
Procurement Due Diligence
Frequently Asked Questions by UK Buyers
Addressing common engineering, tariff, tolerance, and operational questions asked by London design offices and commercial buyers.
How do your deep drawing dimensional tolerances compare to UK engineering standards?
Our tooling is built to precision DIN ISO 2768-m or fine (-f) tolerances. For critical cylindrical diameters, deep drawn shells hold ±0.015mm (±0.0006 inches). Flange flatness, edge straightness, and concentricity are checked using 3D automated Coordinate Measuring Machines (CMM) calibrated to UKAS-equivalent standards.
What is the typical lead time from CAD models to first-article parts in London?
Rapid prototyping via soft tooling or single-stage test dies takes 10 to 15 working days. Progressive mass-production tooling typically requires 25 to 35 days, including complete tool trialing. Pre-production First Article Inspection Reports (FAIR) are air-shipped to London via DHL/FedEx within 48 to 72 hours for client sign-off.
How do you handle post-Brexit UK Customs, UKCA marking, and DDP shipments?
We work with UK-specialized freight forwarders offering complete Delivered Duty Paid (DDP) options directly to your London facility. We manage the UK Import Declaration (CDS), commodity classification codes (HS 732690 / HS 761699), and provide relevant material declarations to assist with your UKCA conformity technical files.
Which materials are optimal for high draw-ratio cylindrical canisters?
Deep Drawing Quality (DDQ) stainless steels—such as 304DDQ and 316L with elevated nickel content (9.5% to 12%)—deliver exceptional ductility and lower strain-hardening rates during multi-step draws. We also routinely form high-purity aluminum alloys (1050/3003-O), cold-rolled strip steels (DC04/DC06), and phosphor bronze (CuSn6).
Can you protect mirror-finished parts from surface scoring during transit?
Yes. We use protective PE or laser-grade PVC barrier films prior to the first draw. After ultrasonic degreasing and final deburring, components are packed in compartmentalized thermoformed trays, anti-static ESD bags, or custom stackable corrugated containers to avoid metal-to-metal contact during sea or air transit.
What technical data is required to receive an accurate tooling and piece-price quote?
Please share your 3D CAD files (STEP, IGES, or SolidWorks) and 2D engineering drawings showing critical dimensions, material specifications, and allowable wall thinning. Include target production volumes and any required secondary operations (beading, tapping, electropolishing, or salt spray testing).
Need Custom Deep Drawn Tooling or High-Volume Stamping?
Connect directly with our applications engineering department. We evaluate draw-depth ratios, suggest blank optimization, and provide transparent tooling quotes within 24 hours.