
- +91-9930498858Call / WhatsApp
- [email protected]Email Us
Explore our advanced precision manufacturing portfolio, spanning deep-drawn micro-enclosures, high-tonnage laser cut stampings, and high-efficiency chemical mass transfer hardware.
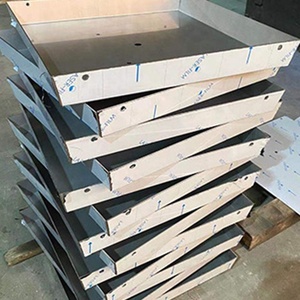
Heavy-duty laser-cut, stamped, and precision-bent sheet components crafted from SS304/316L for high structural stability and anti-corrosion applications.
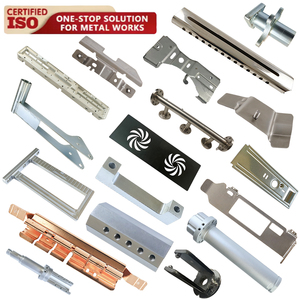
Seamless deep-drawn steel and aluminum cylinders, canisters, and pressure enclosures engineered via multi-stage hydraulic forming for high integrity.
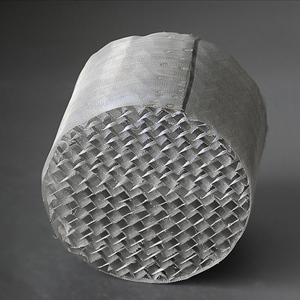
Precision corrugated wire mesh elements designed for ultra-low pressure drop, maximum theoretical stages, and high-vacuum petrochemical distillation.
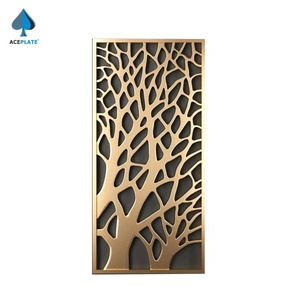
Architectural and acoustic perforated panels punched with high-speed CNC tooling, featuring custom aperture geometries and robust surface finishes.
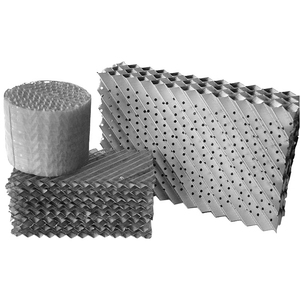
Durable, wear-resistant 304/316 woven metal wire gauze engineered for heavy liquid loading, deep-bed filter applications, and extended operational lifespans.
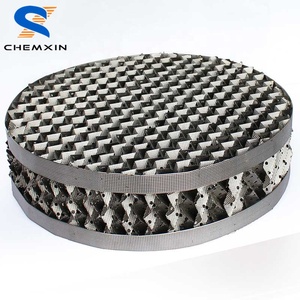
High-efficiency mass transfer corrugated packings offering high specific surface area, reduced hold-up, and uniform vapor-liquid distribution.
Optimized for aggressive chemical towers, fine chemical fractionation, and pharmaceutical processing requiring zero catalytic poisoning and rapid drainage.
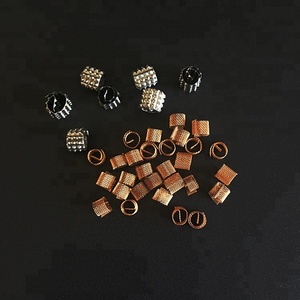
High-precision stamped stainless steel Dixon rings providing maximum liquid spreading and efficiency in small-diameter laboratory columns.
Precision stamping of modern sheet metal alloys—ranging from standard SS304/SS316L austenitic stainless steels to high-nickel superalloys such as Hastelloy C-276, Monel 400, and Inconel 625—requires sophisticated metallurgical control. In high-speed progressive die tooling, the predominant engineering challenge centers on mitigating anisotropic springback, shear edge micro-cracking, and localized work hardening. As an authoritative OEM partner, our manufacturing workflows integrate FEA-based dynamic draw-die simulations that accurately model the Bauschinger effect and yield locus shifts before hard steel is milled.
When producing multi-axis formed stampings and seamless deep-drawn canisters, radial stress fields must be balanced with calibrated blank-holding pressures. Without exact blank-holder force modulation, high-strength alloys rapidly exhibit wrinkling along flanges or tearing at the drawing radius. By applying closed-loop hydraulic and servo-mechanical multi-stage drawing, we achieve uniform wall-thickness reductions within ±0.015mm across deep cylindrical profiles, minimizing secondary annealing cycles and dramatically reducing cycle times for global supply chains.
| Metal Alloy Grade | Yield Strength (MPa) | Formability Factor (r-value) | Work-Hardening Exponent (n) | Best Fit OEM Applications |
|---|---|---|---|---|
| Austenitic SS304/304L | 215 – 240 | 1.05 – 1.20 | 0.45 | Sanitary foodware, heat exchanger plates, column trays |
| Marine Grade SS316/316L | 220 – 260 | 1.00 – 1.15 | 0.40 | Offshore valve seats, structured gauze, chemical vessels |
| Inconel 625 / 718 | 415 – 550 | 0.85 – 0.95 | 0.30 | Aerospace heat shields, gas turbine seals, harsh reactors |
| Monel 400 Alloy | 240 – 350 | 0.90 – 1.10 | 0.32 | Brine marine pump bodies, hydrofluoric acid internals |
| 5052 / 6061 Aluminum | 130 – 275 | 0.65 – 0.85 | 0.16 – 0.22 | EV battery enclosures, architectural lightweight panels |
To support high-reliability procurement, our tool-and-die workshop operates high-precision Sodick Wire EDM cutting and AgieCharmilles 5-axis CNC machining centers. Progressive stamping dies are manufactured with tungsten-carbide inserts (grade CD-650 or equivalent) in high-wear shearing stations, preserving dimensional integrity and burr heights below 5% of material stock thickness over million-stroke production cycles.
Procurement directors and supply chain managers face volatile commodity pricing, regulatory shifts, and ESG audits. Discover where high-precision contract manufacturing is heading through 2030.
Global OEMs are transitioning from single-source dependencies to resilient dual-sourcing strategies. Sourcing from experienced export fabricators with direct port access and automated warehousing lowers supply chain exposure by over 40%.
Stringent aerospace and automotive audit trails now mandate digital material tracking. Procurement contracts require EN 10204 3.1 certification, XRF spectrographic validation, and continuous CMM dimensional inspection mapped directly to each heat batch.
Driven by Scope 3 carbon mandates, engineering teams prioritize stamping suppliers that run nested blank nesting algorithms and high-speed servo-press scrap minimization systems, achieving material utilization rates upward of 88%.
The high-precision stamping landscape is shifting from traditional mechanical flywheel flypress systems toward programmable CNC servo presses. By enabling tailored slide-motion kinematics—such as pendulum mode, coining dwells, and vibration-assisted deep drawing—servo drives minimize internal residual stresses and yield smoother sheared surfaces in high-strength steels. This advance reduces post-stamping grinding, tumbling, and edge-deburring operations.
Simultaneously, zero-defect quality programs rely on in-die optical inspection. High-resolution telecentric lens cameras integrated directly into die strip-exit stations continuously verify pilot hole centerlines, hole circularity, and burr formation at speeds exceeding 600 strokes per minute. AI-driven vision engines detect micro-galling or broken punches in real time, preventing full production batches of out-of-tolerance parts and providing transparent statistical process control (Cpk ≥ 1.67) directly to corporate engineering teams.
Refined over 25+ years of continuous manufacturing and delivery to 20+ countries across North America, Europe, Australia, and the Middle East.
Direct mill relationships guarantee verified mechanical parameters and chemical compositions. Every batch is certified with complete EN 10204 3.1 heat traceability.
From progressive dies to deep-draw stages, our tooling is designed, engineered, and maintained in-house using ultra-precise CNC wire EDM and multi-axis milling.
Rigorous pre-shipment dimensional inspections using calibrated CMMs, optical profile projectors, and surface roughness testers, accommodating independent third-party inspections.
Heavy-duty, fumigated timber crating, anti-corrosive VCI packaging, barcoded palletizing, and streamlined customs clearance documentation prepared for over 20 nations.
Critical technical, operational, and commercial answers for purchasing managers, tool engineers, and industrial designers.
Tooling fabrication typically requires 3 to 5 weeks depending on die complexity, progressive stage count, and part geometry. Upon tool sign-off, First Article Inspection (FAI) samples and comprehensive CMM bubble inspection reports are delivered within 5 business days for client approval.
All progressive stamping and deep drawing tooling includes lifetime preventative maintenance under active production contracts. We track cycle counts digitally, schedule sharpening of punch and die steel inserts, and replace wear components with zero amortized cost to the buyer.
Please supply 2D engineering drawings (PDF/DWG format with geometric dimensioning & tolerancing), 3D native CAD files (STEP, IGES, or Parasolid), required alloy grade specifications, surface finishing treatments, estimated annual volume (EAV), and batch shipping requirements.
Our fabrication floor incorporates deburring, CNC spot and TIG welding, passivating, electro-polishing, ultrasonic washing, bead blasting, heat treatment (stress relieving/annealing), powder coating, and specialized cleanroom anti-static packaging for sensitive electronic or vacuum assemblies.
Send your CAD files or process data sheets today for DFM analysis and competitive factory-direct pricing from our engineering team.