- +91-9930498858Call / WhatsApp
- [email protected]Email Us
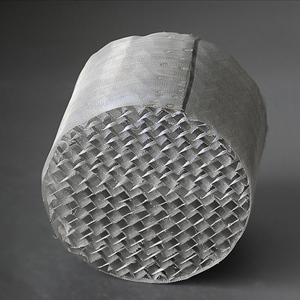
In modern industrial process engineering, the perforated filter core represents the primary structural backbone in liquid-solid, gas-solid, and vapor-liquid mass transfer systems. Serving as the inner support tube or outer reinforcement basket, a filter core must withstand severe hydraulic surges, aggressive thermal cycling, and acidic corrosive dynamics without structural collapse or open-area distortion. As an experienced precision manufacturer and exporter since 1998, we supply fully certified OEM column internals, perforated tubes, and woven wire matrix cores engineered to ASME, ISO, and DIN specifications.
Explore our integrated selection of custom-formed filter cores, distillation column internals, wire gauze assemblies, and metal stampings manufactured for mission-critical operations.
A comprehensive assessment of weld integrity, collapse rating, and fluid dynamics under continuous operational stress.
The structural load on a filter core rises exponentially when filtration media accumulates particulate cake. Our perforated cores undergo precise finite element analysis (FEA) to calculate the critical collapse pressure based on tube diameter, sheet gauge, margin allowance, and seam integrity (spiral TIG, longitudinal seam, or resistance welded lock seams).
Balancing open flow area against structural rigidity is critical. A 30% to 50% staggered perforation layout optimizes flow velocity while minimizing flow turbulence and localized pressure drops (ΔP). Burr-free punching prevents media damage during cartridge pleating or wire mesh wrapping.
Fabricated in 304/304L, 316/316L, and exotic superalloys including Hastelloy C-276, Monel 400, and Inconel 625. Our full chemical annealing and electropolishing services eliminate carbide precipitation and maintain corrosion resistance in sour gas, marine brine, and high-purity chemical processing.
| Alloy Grade | Standard Yield Strength (MPa) | Recommended Open Area (%) | Joining Methodology | Target Industry Application |
|---|---|---|---|---|
| AISI 304 / 304L | 215 – 240 | 28% – 42% Staggered | High-Frequency TIG / Seam Weld | Standard Hydraulic & Lubricant Filtration |
| AISI 316 / 316L | 220 – 290 | 30% – 48% Staggered | Plasma / Laser Seam Welding | Chemical Processing & Marine Desalination |
| Hastelloy C-276 | 355 – 390 | 22% – 36% Custom Matrix | Automated Micro-Plasma TIG | Petrochemical Sour Service & Wet Cl2 Gas |
| Inconel 625 | 415 – 460 | 25% – 40% Perforated Slot | Orbital GTAW Precision Weld | High-Temperature Aerospace & Nuclear Steam |
| Duplex 2205 | 450 – 520 | 32% – 45% Round Staggered | Pulsed TIG with Matching Filler | Offshore Hydrocarbon & High-Chloride Brine |
Strategic purchasing benchmarks shaping global supply chains through 2026–2030.
Traditional mechanical punching often introduces micro-burrs and edge work-hardening. Global buyers are transitioning toward fiber laser tube perforation and CNC micro-slotted tubes. This guarantees pristine inner core surfaces that prevent fine pleated non-woven filter fabrics from tearing under cycling differential pressures.
Due to stricter refinery safety and ESG mandates, international procurement policies now demand end-to-end metallurgical verification. Each perforated filter core must map directly to its master melt heat number via optical emission spectroscopy (OES) and positive material identification (PMI) documentation.
Engineers are increasingly specifying high-integrity stainless steel cores that support repeated chemical cleaning and back-pulsing cycles over 10 to 15 years, moving away from single-use disposable synthetic housings and lower-spec plastic cores.
Combining 25+ years of Indian manufacturing heritage with global export compliance.
From sheet decoiling, precision punching, spiral roll forming, to deep drawn stamping of custom end caps, our integrated engineering avoids multi-tier subcontractor overhead, providing direct factory lead times and consistent mechanical tolerances.
Our deep competence extends beyond filter cores to comprehensive column internals, structured packing, random packing rings, and custom wire mesh weaves. We help EPC contractors source matched fluid-separation packages from a single qualified vendor.
Serving plants throughout the USA, UAE, Saudi Arabia, Australia, Canada, and Europe with seaworthy wooden crate packaging, vapor corrosion inhibitor (VCI) preservation, and pre-cleared customs documentation.
Authoritative answers addressing design margins, hydraulic parameters, and quoting specifications.
To provide an exact engineering design and quotation, provide the outer diameter (OD), total length, wall thickness/gauge, perforation geometry (hole diameter, pitch, and staggered vs. straight pattern), material alloy grade, end termination design (plain cut, beaded, flared, or stamped end cap), and estimated maximum differential collapse pressure (ΔP).
Spiral welded perforated tubes distribute hoop stress continuously along a helical seam rather than focusing stress across a single longitudinal line. This design yields significantly higher burst and collapse resistance under elevated pressure cycling, making it ideal for deep well screens, high-viscosity oil filters, and high-pressure chemical scrubbers.
Yes. Our precision CNC punching lines can program custom solid margins at both ends or along designated longitudinal zones. Solid end margins are critical for secondary operations such as automated end-cap welding, elastomeric bonding, threading, or gasket seating.
Depending on process purity standards, we apply ultrasonic degreasing, mechanical centrifugal deburring, glass-bead blasting, chemical passivation (ASTM A967), or commercial electropolishing to ensure internal and external surfaces are completely free of burrs and contaminants.
Yes. We regularly coordinate inspections with agencies such as SGS, Bureau Veritas, DNV, and TUV. Complete EN 10204 3.1 material test certificates, dimensional inspection records, and weld penetration testing reports accompany every export dispatch.
Send your 2D/3D CAD drawings or process data sheets directly to our metallurgical engineering team for rapid feasibility review and competitive volume pricing.